The aluminium windows and doors factory
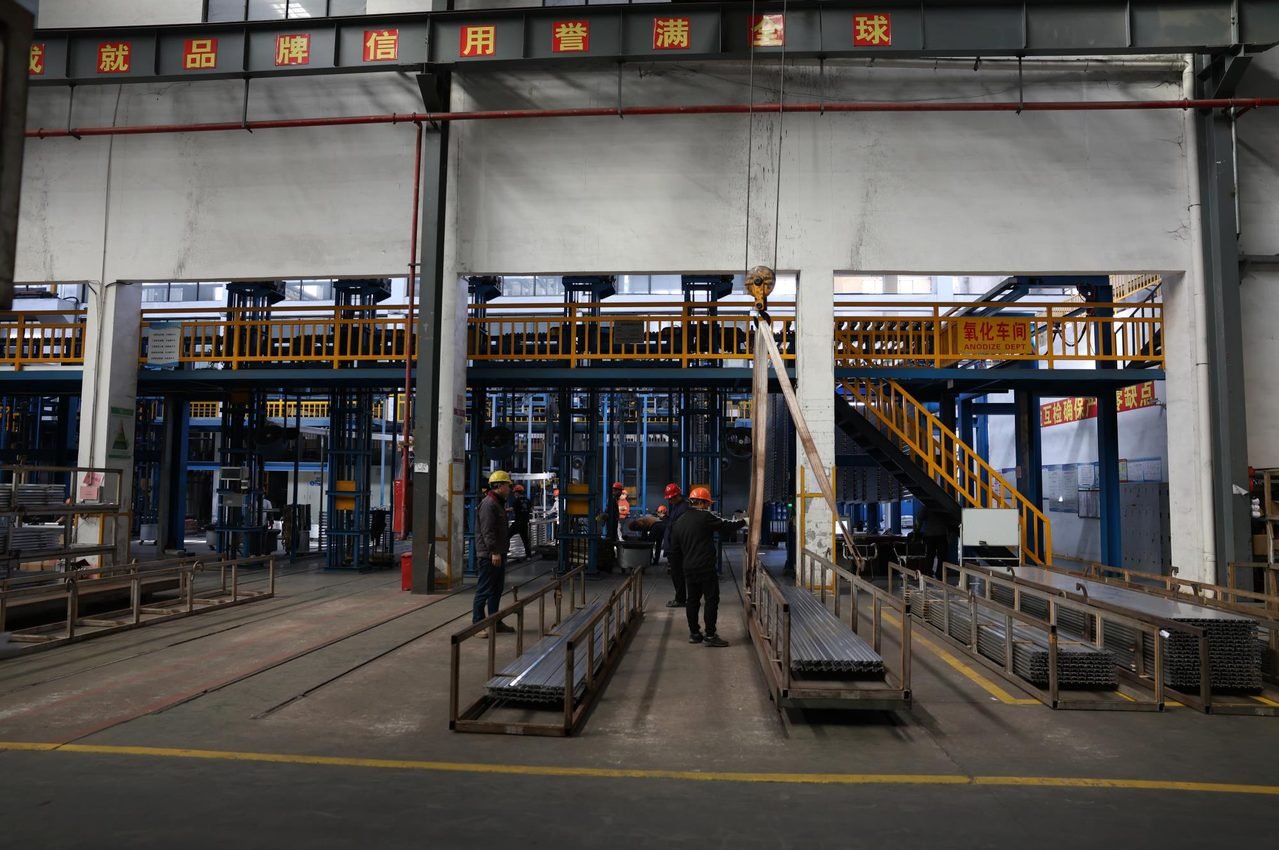
One site, one quality gate — the factory behind every system on the line card.
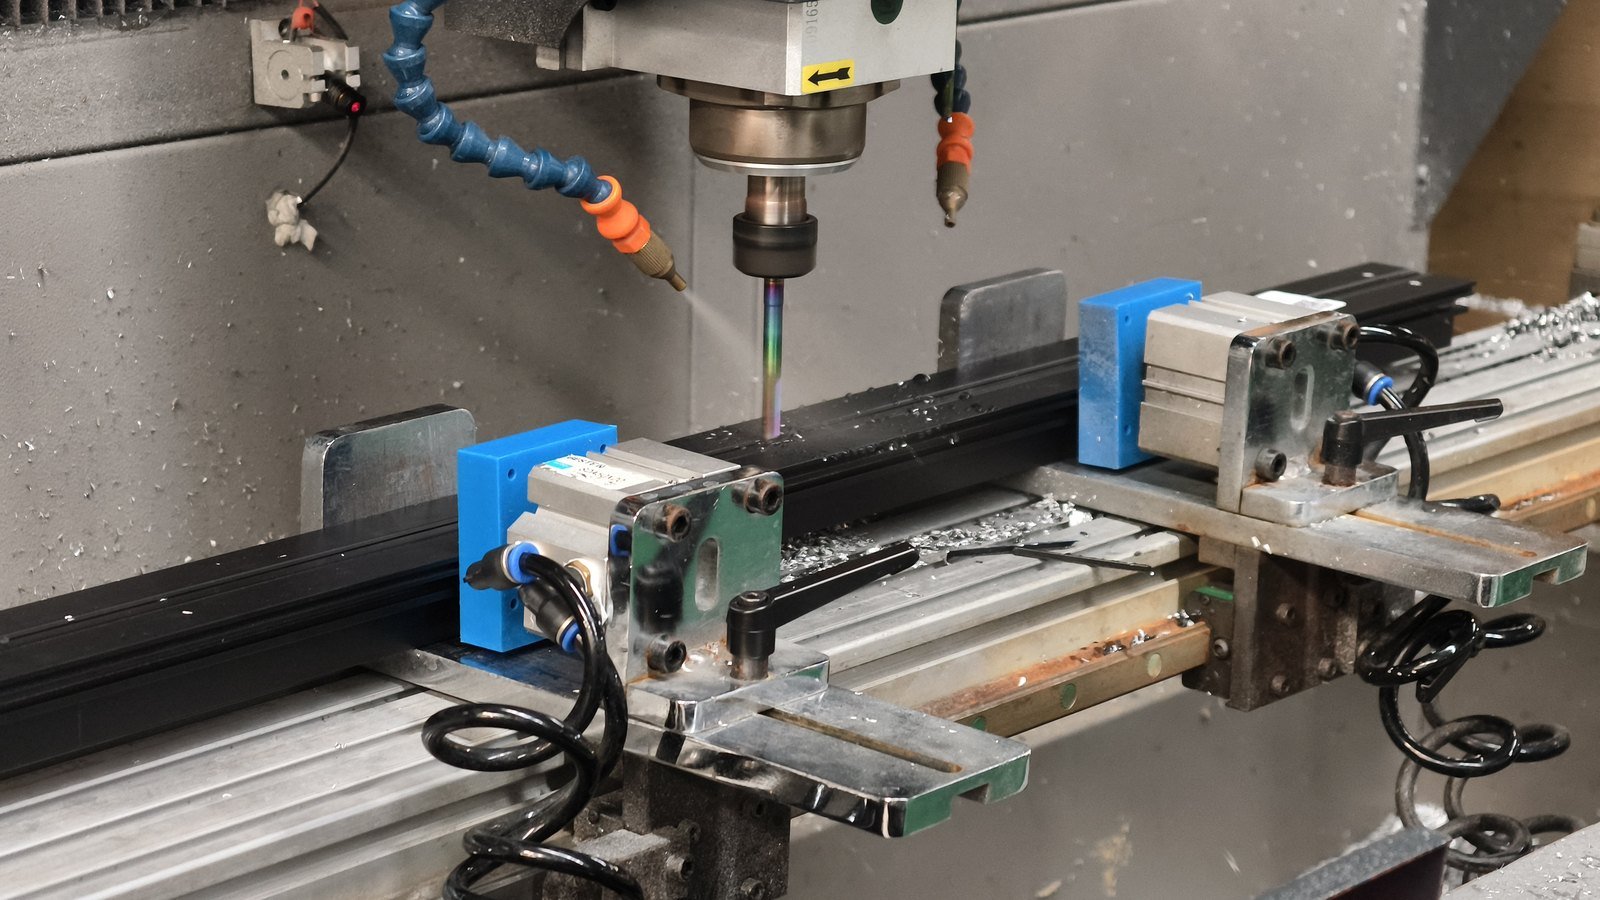
Sashes leave the line factory-assembled and pre-glazed — the tolerance work is done under a roof, not on your job site.
The factory sits inside a Foshan building-materials group founded in 2006. Who the company is, what it holds and how the division is structured is set out on the about the factory division, including the group registration details and the product scope each entity covers.
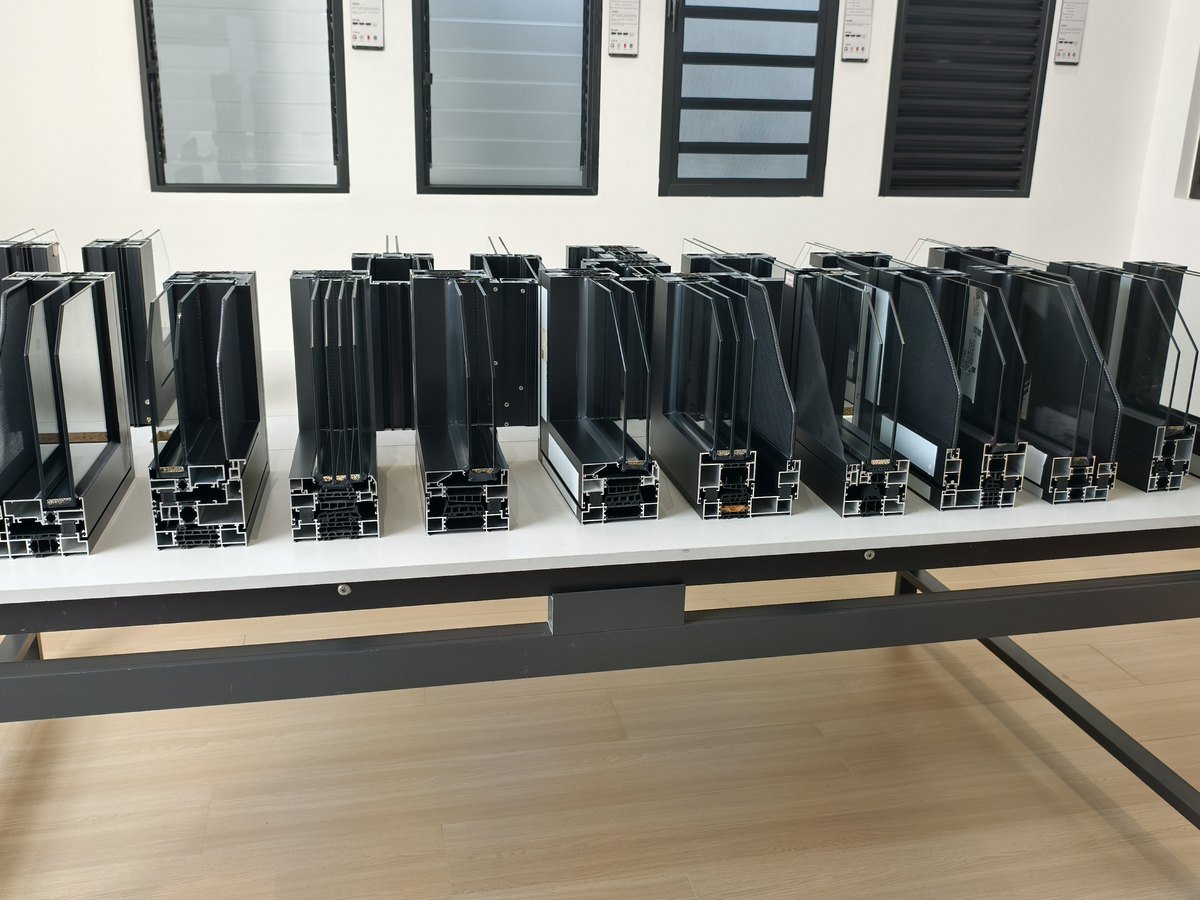
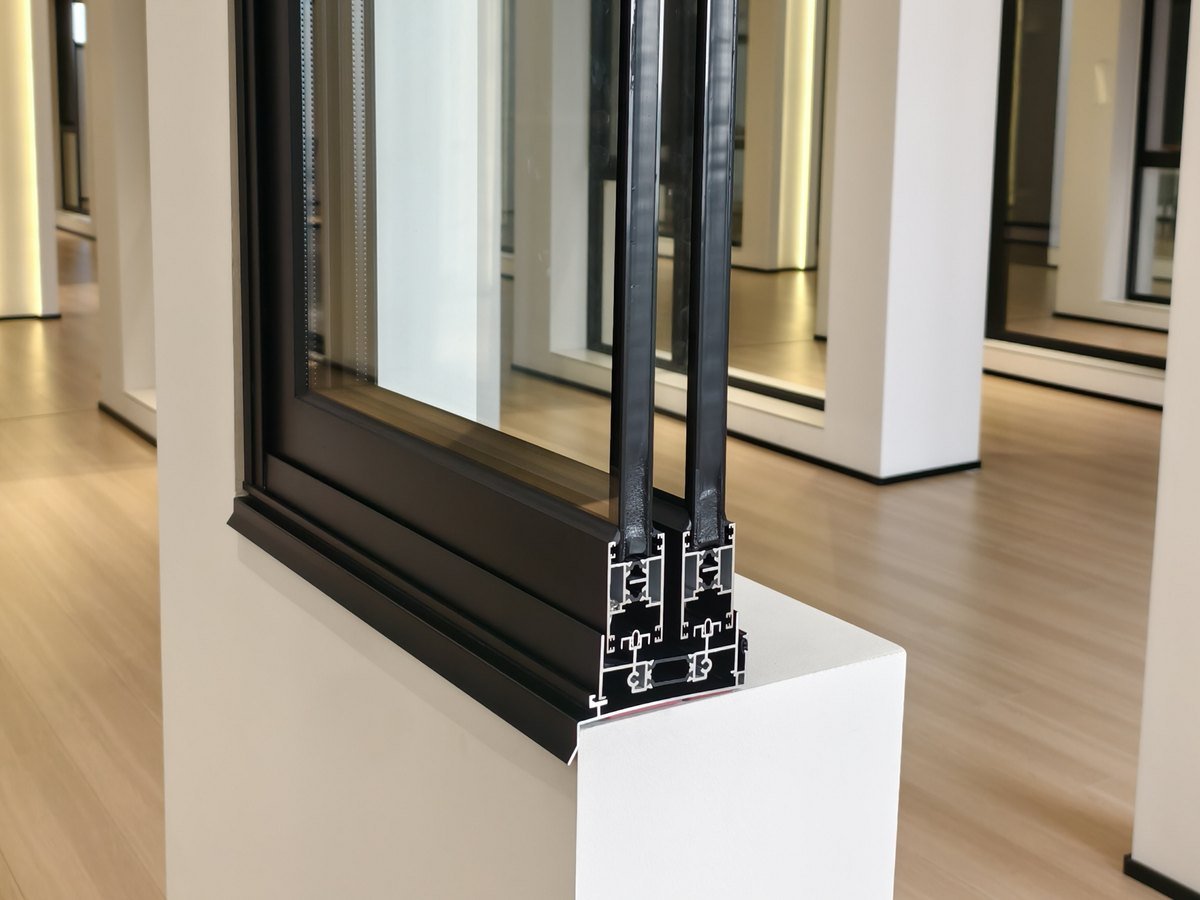
The section, up close
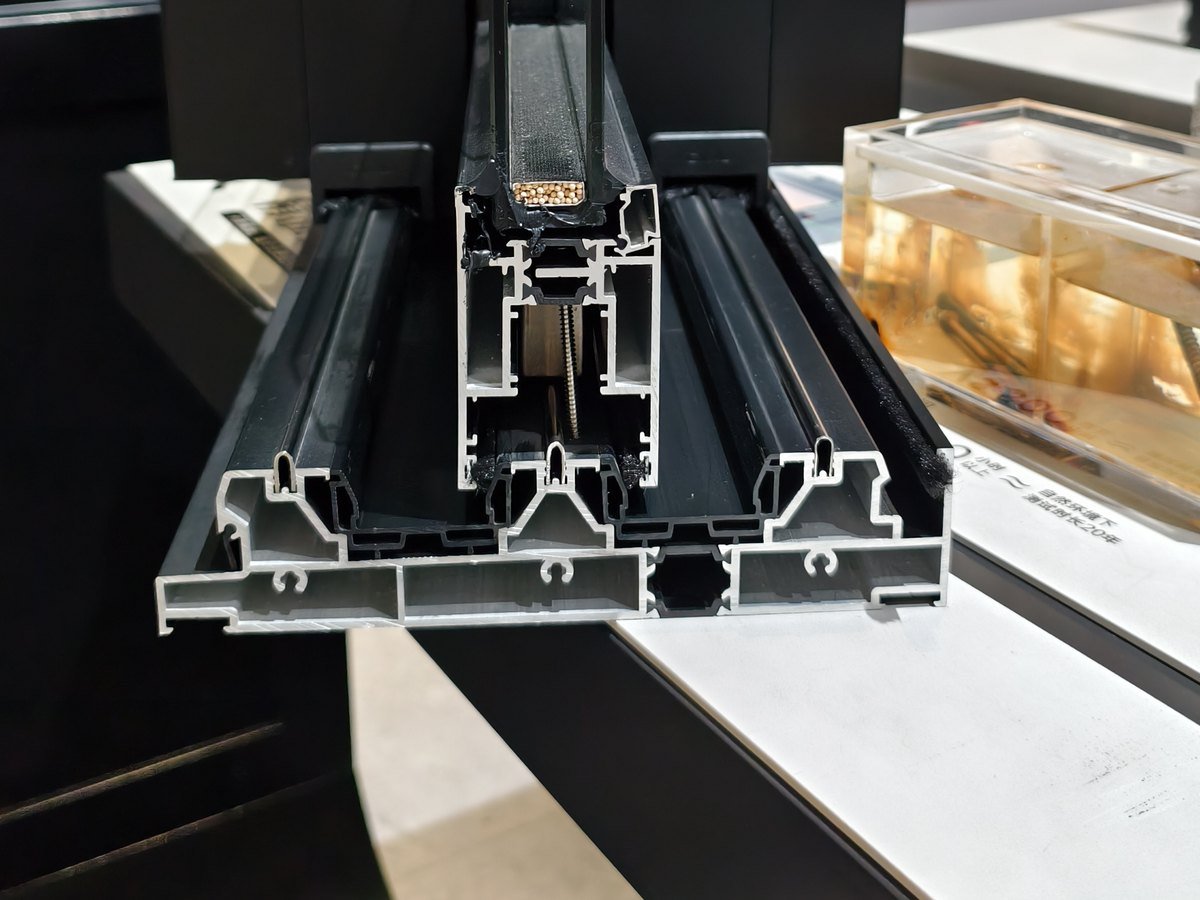
Every system is built on multi-chamber 6063-T5 extrusion with a continuous PA66 thermal-break bar and two replaceable EPDM gasket lines. The values in the performance band on the home page are read off this section — here it is, photographed.
Materials, specified at the line
Every material below is stated on the data sheet per project — the mill certificate for the profile, the schedule for the coating, the specification for the glass. Nothing is “equivalent or better” in the paperwork; the paperwork names the material.
Profile
6063-T5 multi-chamber extrusion, PA66-GF25 thermal-break bar, corner-bonded in the press line. Mill certificate retained per heat.
Surface
Chromate-free pre-treatment, 80–100 µm powder coat with the salt-fog schedule on coastal elevations, anodising or wood-grain film where the specification calls for them.
Glazing
Tempered, laminated or IGU to the project schedule — 0.38 SGP interlayer on impact units, 24–42 mm asymmetric laminated core on the acoustic range.
Hardware & seals
316 stainless on marine schedules, 6–12 point multi-point locks, anti-lift cam on every sash, two replaceable EPDM gasket lines with the replacement cycle published.
Six stages, one gate
- 01
Extrusion & thermal break
- 02
Finishing
- 03
Glazing
- 04
Sash assembly
- 05
Quality gate
- 06
Crating & loading
The quality gate, in numbers
Spot-tested on the rig at stage five, and the tested figure — not the nominal one — is what lands in the data sheet. Configuration targets as published on the home page.
1.4 W/m²K
3,500 Pa
900 Pa
Class 4
45 dB
The ten shop-floor operations →Quality control checkpoints →Packing and container loading →
What every crate documents
The balance of payment runs against a photo report, and the report runs against the same documentation that ships in the crate. Nothing on site should be guessed.
Packing list & loading report
Unit-by-unit, per container, with the crate and pallet map.
Pre-shipment photo report
Every unit photographed at the quality gate before the balance is due.
Hardware & glass schedules
The exact lock set, hinge line and glazing unit per reference — matches the schedule.
Install guide per market
The three-zone fixing detail and sealant schedule for your building code.
Crating
Corner-protected, desiccanted, with a moisture card at the first layer.
What a buyer should verify — and where we show it
The list below is what we would ask of a supplier. Each row names the document we issue against it, so the audit takes a checklist, not a conversation.
“Is the profile the one on the data sheet?”
Mill certificate per heat, attached to the shop drawings.
“Is the coating schedule specified, not assumed?”
Coating data sheet with the salt-fog hours for your elevation, per project.
“Is the glass unit built to the schedule?”
Glazing schedule per reference — thickness, core, SGP, low-E — matched against the quotation.
“Was the rating tested on our sizes?”
Project test report (PGT for impact, EN/AS rig for performance) on the configuration we ship.
“Does the documentation follow the container?”
Packing list, loading report and pre-shipment photo report — the balance runs against them.